1. Understand the names before comparing materials
EVA is ethylene-vinyl acetate. PE is polyethylene. PP is polypropylene. These names identify the polymer, not a complete foam specification.
EPE, expanded polyethylene, belongs to the PE family. In conventional packaging trade usage it commonly describes non-crosslinked extruded sheet, roll or plank foam. XLPE/XPE and IXPE describe crosslinked PE forms. Suppliers also offer bead-based PE materials, so ask for the exact form and grade when the label is ambiguous. Sealed Air describes Ethafoam planks as non-crosslinked PE; Zotefoams describes Plastazote as crosslinked PE. Both are PE foam. Ethafoam, Plastazote
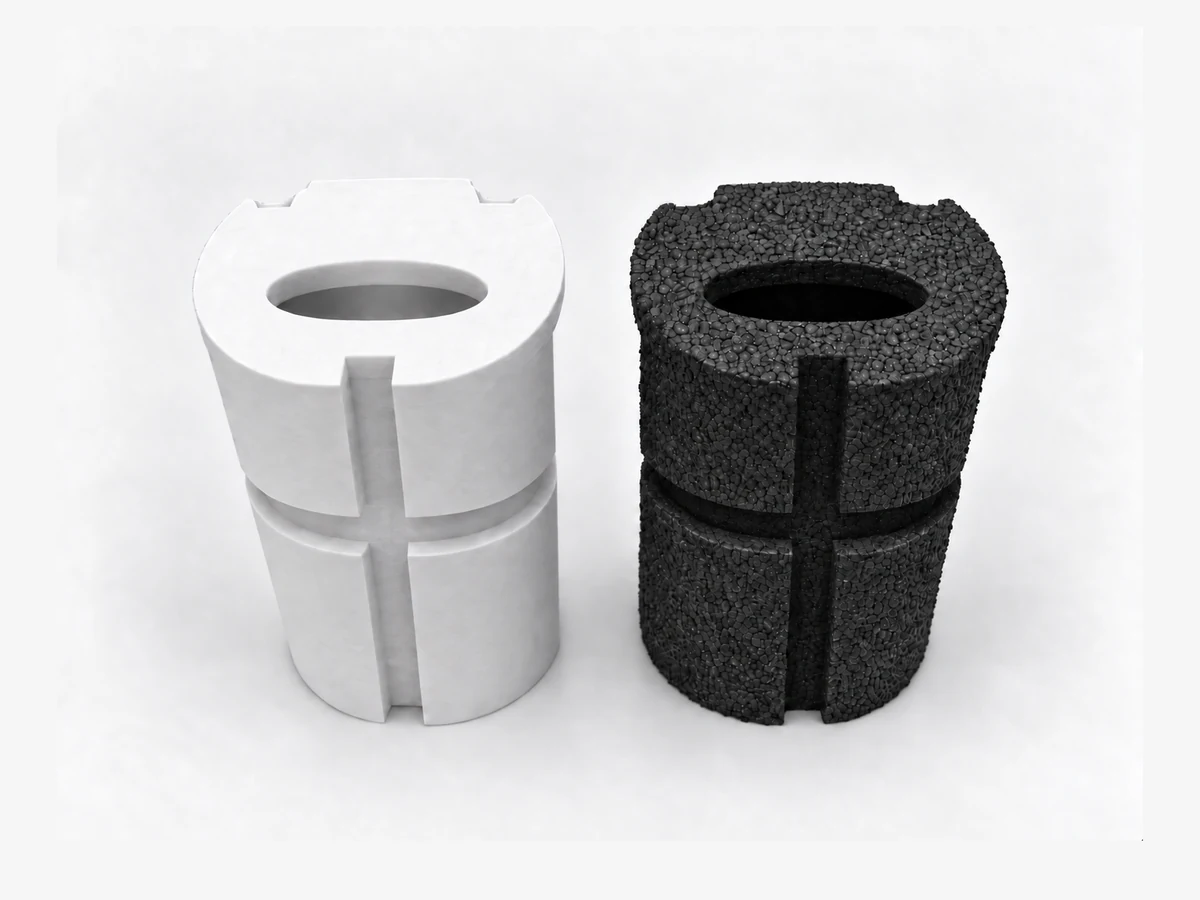
EPP, expanded polypropylene, belongs to the PP family and is commonly supplied as beads consolidated into moulded parts or blocks. PP also exists as crosslinked sheet foam for liners and formed components. Toray describes both PE- and PP-based sheet foams; ARPRO documents EPP moulded parts. Toray, ARPRO
The comparison below therefore separates useful commercial forms. It does not treat PE/EPE or PP/EPP as unrelated polymers.
2. Material comparison
| Material/form | Reasons to consider it | Trade-offs and open checks | Potential customer applications |
|---|---|---|---|
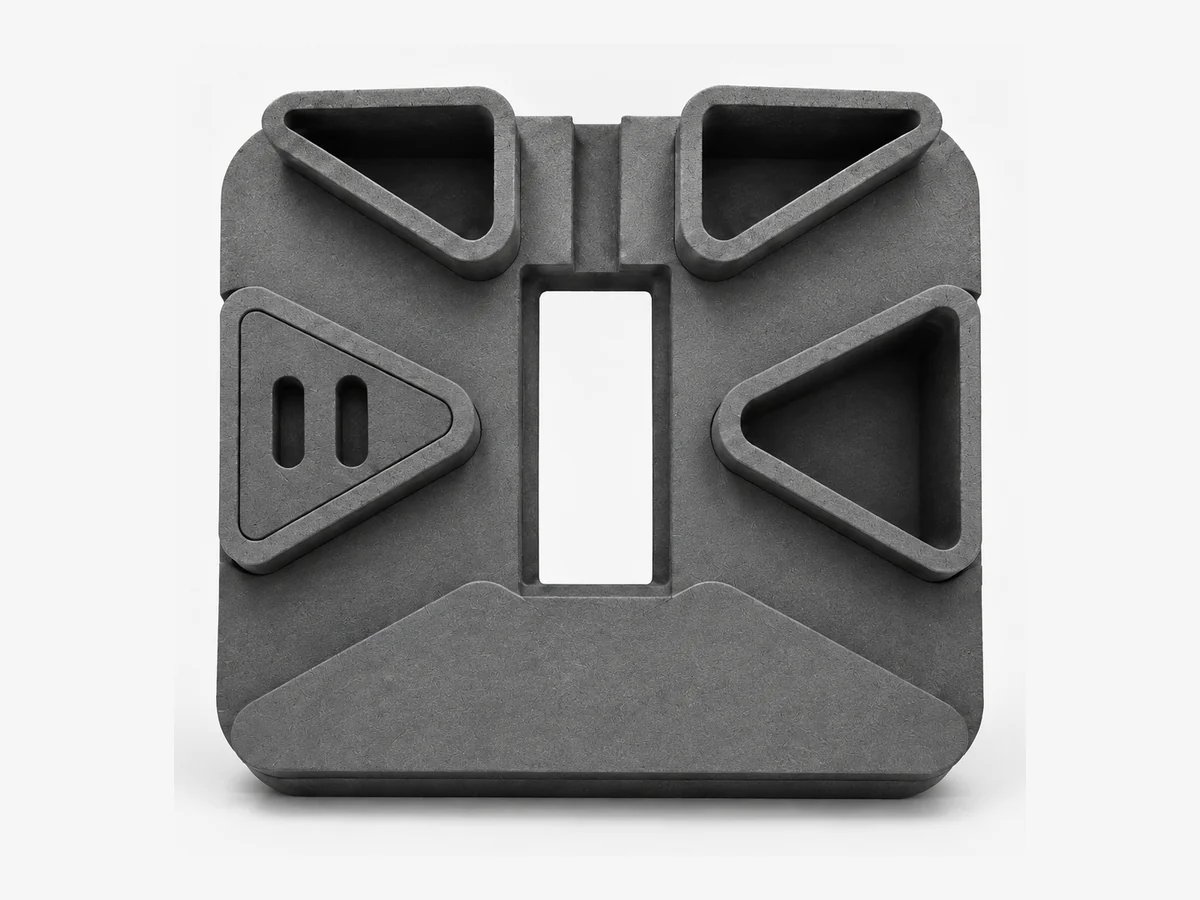
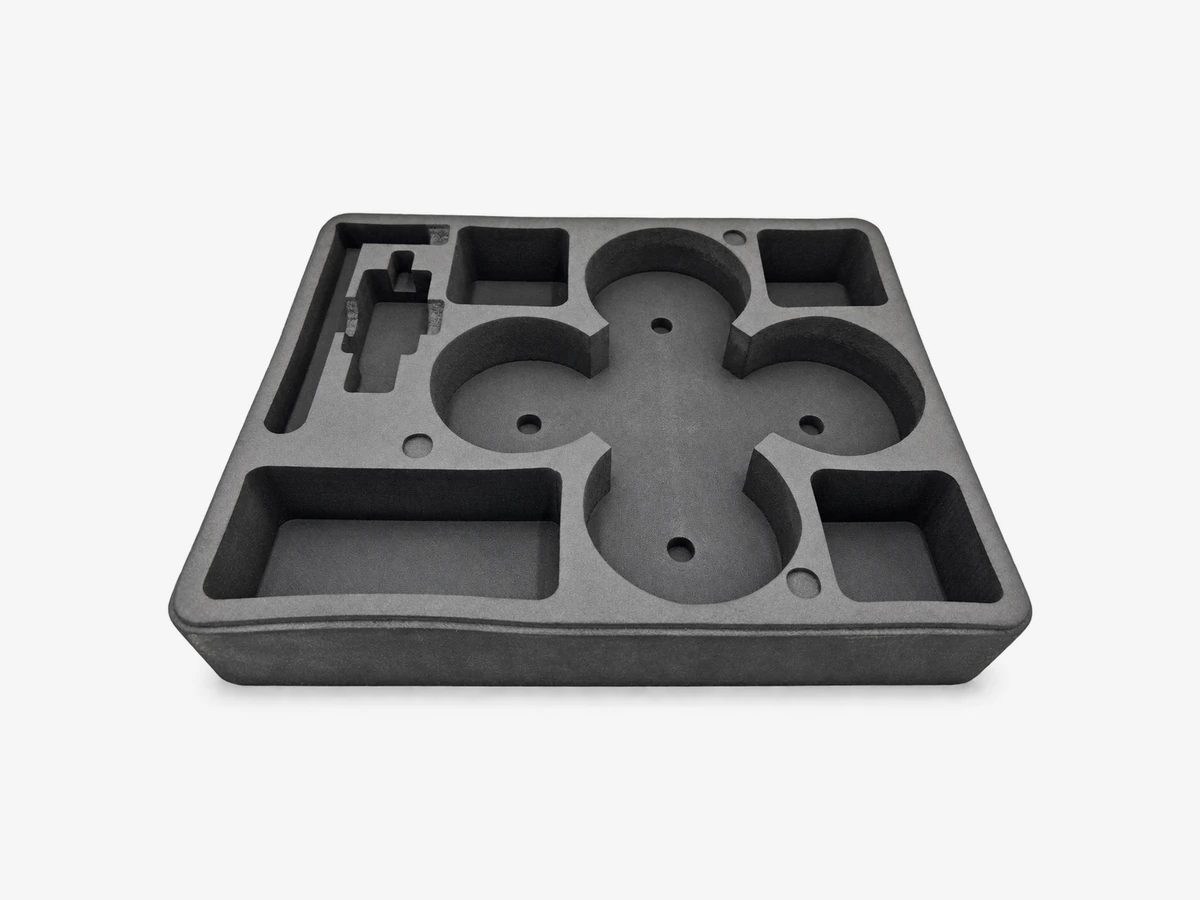
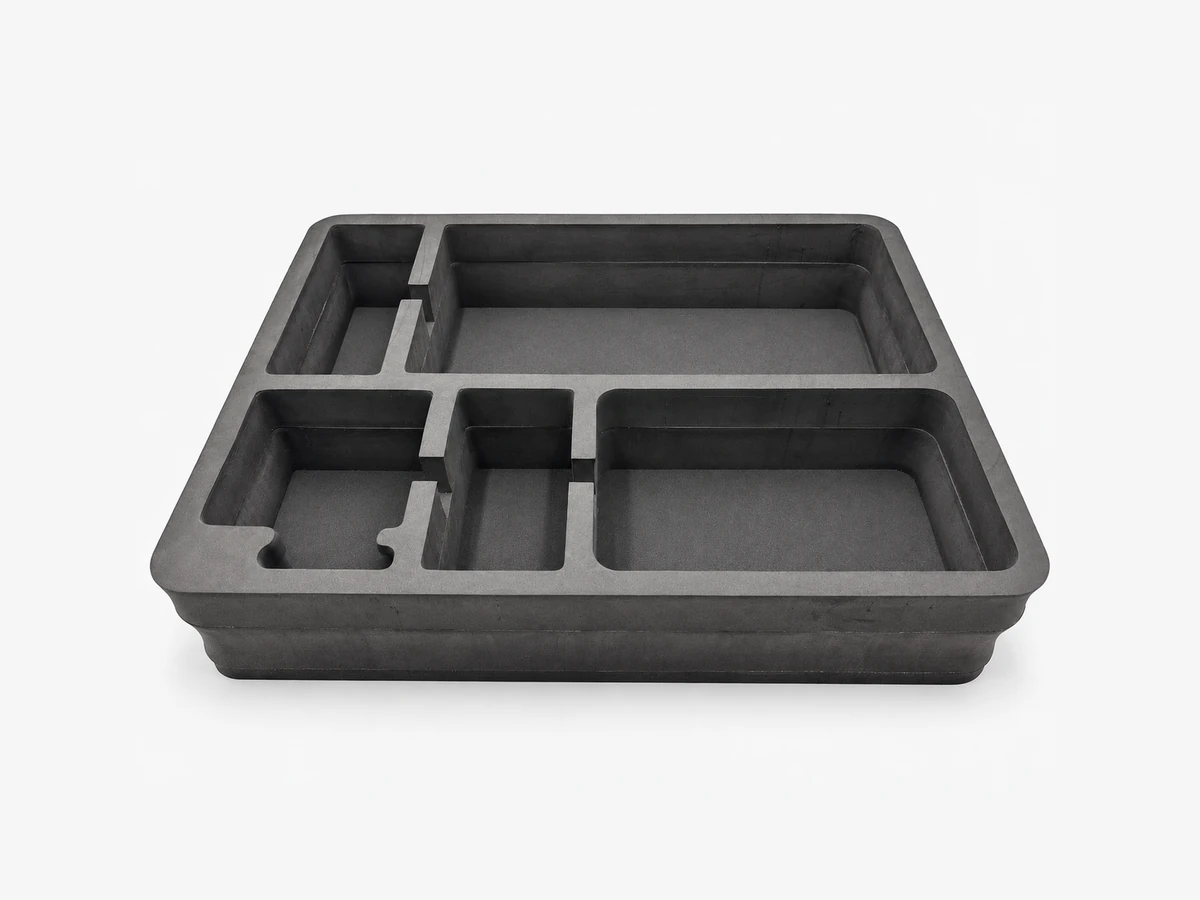
| EVA foam, commonly closed-cell crosslinked sheet/blockCompare the grade and design | Resilient cushioning; shaped, machined or layered supports; tactile finish options | Check compression, long-term fit, temperature and adhesive. ESD/FR require a specific grade. Compare finished cost rather than assuming all EVA is premium or expensive | Detailed drone and tool inserts, cable supports, equipment liners, formed cases and backpack interfaces |
| PE foam, especially XLPE/IXPECompare the grade and design | Crosslinked forms for cut inserts, liners and repeatable component separation; many grade choices | “PE” alone leaves cell structure, compression and surface finish unspecified. Bonding and environmental behaviour require review | Instrument cases, electronic equipment supports, panels, separators and protective liners |
| Conventional EPE, non-crosslinked PE sheet/roll/plankCompare the grade and design | Simple surface wraps, pads, spacers and fabricated cushioning; extruded plank grades also serve repeat-use packaging | Thin wrapping foam is not interchangeable with a load-bearing plank. Verify durability, pocket detail, creep and required foam volume; low density alone does not prove lowest delivered cost | Shipping end caps, protective sleeves, industrial equipment pads and returnable dunnage using suitable plank grades |
| PP sheet foam, including crosslinked formsCompare the grade and design | Formed liners and components; investigate heat-resistant grades where relevant | Specify the actual PP-based grade. Forming, stiffness, bonding and service temperature differ across products; sheet foam is not EPP bead foam | Interior trim, equipment liners, formed padding and insulation components |
| EPP bead foamCompare the grade and design | Lightweight shaped supports; repeated-impact energy management; reusable transport structures | Moulded geometry requires tool/process review. Bead size and fusion influence small features and finish. Confirm final part density, local loads and grade properties | Reusable trays, returnable industrial packaging, insulated transport bodies and shaped equipment cradles |
These starting points combine supplier descriptions with proposed engineering applications. EVA resilience is described by Zotefoams; low-density surface wrapping by Sealed Air Cell-Aire; PP sheet applications by Toray Plastics America; EPP properties by ARPRO. Suitability still depends on the chosen grade and design.
3. Density is one part of the specification
Density describes mass per volume, normally kg/m³. A part retaining one litre of foam at 70 kg/m³ contains approximately 70 g of foam, before adhesive, skins or other components. Calculate retained foam volume after pockets and holes are removed.
Useful conversions: 1 g/L = 1 kg/m³; 1 lb/ft³ ≈ 16.02 kg/m³. For EPP, distinguish the bulk density of loose beads from the density of the finished moulded part. ARPRO lists these separately. ARPRO Black grade information
Specific examples, not universal family ranges
| Example | Documented density | What this demonstrates |
|---|---|---|
| Existing FFG EVA examples | 70 kg/m³, with 35 Shore C hardness | Density and hardness are separate specifications; these values describe the examples, not all EVA |
| Zotefoams Evazote EV50 | Nominal 50 kg/m³ | Another EVA grade can have different mechanical data |
| Zotefoams Plastazote LD33 | Nominal 33 kg/m³ | Crosslinked PE also requires a specific grade definition |
| Sealed Air Ethafoam brochure grades | 1.5–9.0 lb/ft³, approximately 24–144 kg/m³ | Non-crosslinked PE plank foam is offered across several densities |
| ARPRO moulded-property table | Example densities 20–200 g/L, equivalent to kg/m³ | EPP mechanical properties vary with finished density |
Supplier examples: EV50 sheet, LD33 sheet, Ethafoam brochure, ARPRO physical properties. Typical datasheet values are not automatically purchasing limits.
What else to specify
| Specification | Why the project needs it |
|---|---|
| Polymer, form, grade and cell structure | Identify what is actually being purchased |
| Density, thickness, dimensions and tolerances | Control mass and fit |
| Hardness, including Shore scale and test method | Compare like-for-like readings; Shore C, A and OO are not interchangeable |
| Compression stress at stated strain | Understand support and preload; density is not a direct stiffness measurement |
| Compression set and creep, with conditions | Review recovery and sustained-load deformation |
| Cushioning data at relevant thickness/load | Develop shock protection around equipment fragility |
| Temperature, exposure time and dimensional change | Check fit and performance across service conditions |
| Water absorption, vapour behaviour and chemicals | Review actual environment and cleaning/adhesive compatibility |
| Electrical properties and test conditions | Define ESD or insulating function correctly |
| Flame test, classification, thickness and grade | Match a real requirement rather than “fireproof foam” |
| Finish, contamination and durability | Check contact with lenses, coatings, moving parts and repeated handling |
For demanding designs, also define tensile/tear behaviour, abrasion, UV exposure, odour/emissions, cleaning agents and any material-contact restrictions. An acoustic absorption or vibration requirement needs its own data: ordinary closed-cell packing foam should not be assumed to be a sound absorber or an isolation mount.
4. Design the foam around the equipment
Interior positioning: drones, electronics and machinery
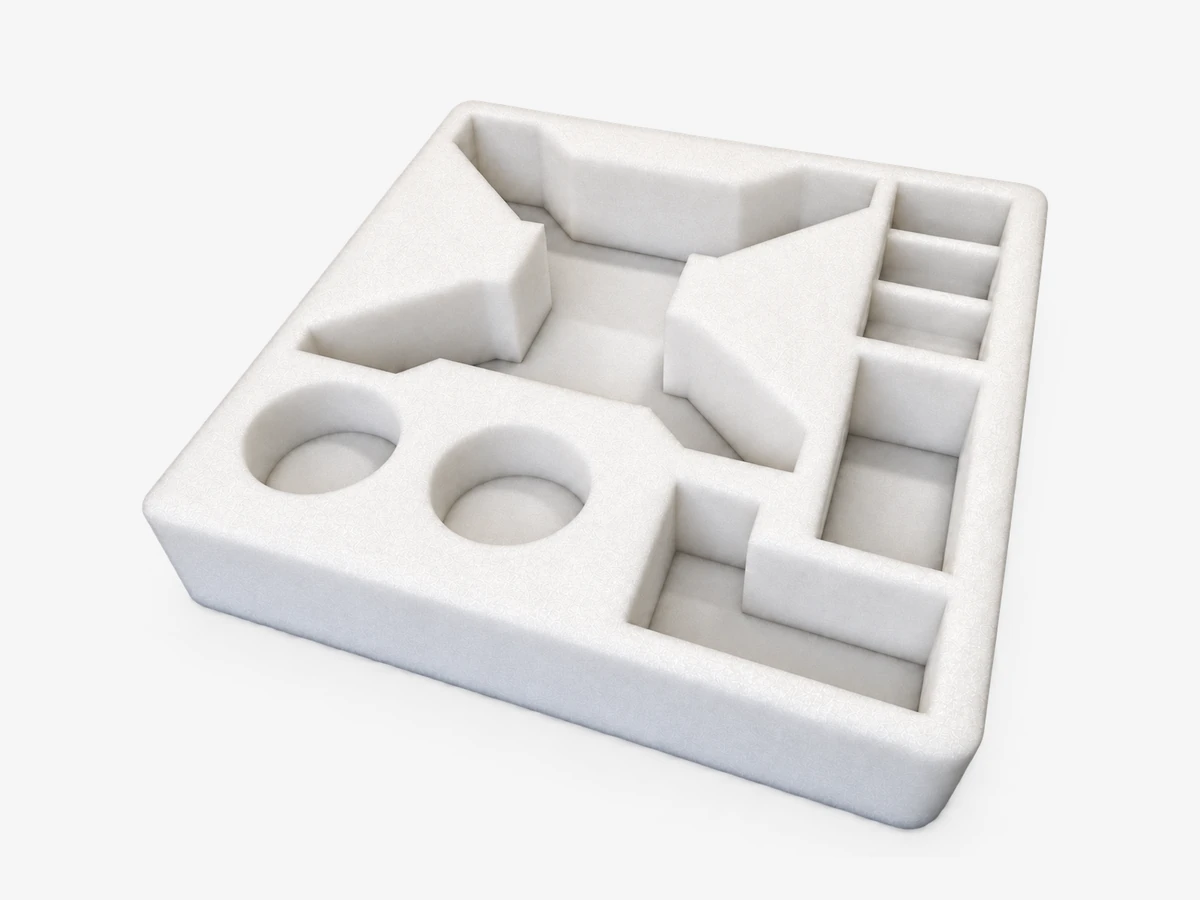
Start with the components to locate, approved contact surfaces, loads and service access. A shaped insert could hold a cable route or support a housing without pressing against fragile connectors or board-mounted parts.
For a powered drone or electronic enclosure, review heat-producing components, airflow and heat-transfer paths before filling empty space. Keep access for inspection and replacement. Check preload, compression recovery, cable bend clearance, vibration, drainage/condensation and possible particles or adhesive emissions. Where radio equipment is involved, review material effects on the antenna environment, especially when conductive additives are proposed.
These are proposed design checks. An insulating support, an ESD packaging insert and a potting compound fulfil different requirements. Conductive foam near exposed circuitry or battery terminals needs electrical clearance review.
Shock and vibration
Choose load-bearing areas, thickness, clearance and foam response using equipment mass, fragility and expected handling. A harder or denser foam is not automatically a better cushion. Ask for relevant cushion curves and then validate the equipment inside its complete package or enclosure. ASTM D1596 describes material cushioning tests and explicitly distinguishes their results from package performance. ASTM D1596
Vibration also needs a separate requirement and check. A tight positioning insert alone does not establish vibration isolation. Agree the operating or transport exposure and an acceptance criterion with the customer.
Moisture and humidity
Closed-cell foam can be useful where limited water uptake is required, but the insert does not by itself control humidity or make an enclosure waterproof. Review seams, joints, coatings and condensation. If an IP rating is required, assess the enclosure design against the applicable test. IEC 60529
Thermal insulation and operating temperature
Insulation can slow heat transfer in a transport container. Temperature-holding time requires the complete box, closure, payload, ambient conditions and any coolant to be defined and tested. In powered equipment, insulation must be reviewed alongside the heat dissipation design.
Compare temperature data for identified grades under the manufacturer’s stated conditions. EV50’s sheet lists 65°C and LD33’s sheet lists 95°C as recommended maxima using a particular 24-hour shrinkage criterion. These figures illustrate different grade data; they are not guaranteed continuous service limits for every geometry or load. EV50, LD33
ESD and flame requirements
For exposed electronics, distinguish low-charging materials, dissipative/conductive behaviour and discharge shielding. Foam colour alone establishes none of these. Transport outside an ESD protected area may require shielding as well as appropriate contact materials. EOS/ESD Association packaging guidance
For flame behaviour, request the applicable test, exact classification, grade, thickness and report. Separate FR and ESD options exist, but the combination must also be confirmed. ARPRO’s documentation shows grade- and thickness-dependent fire tests; a foam result does not qualify an entire device or battery assembly. ARPRO specialty grades, ARPRO fire tests
5. Choose the fabrication route with the geometry
| Process | Useful starting point | What to review |
|---|---|---|
| Band saw cutting | Blocks, straight cuts and accessible profiles in suitable slab foam | Blade/fixturing, cut finish, compression during cutting and feature access |
| Die cutting | Repeated through-cut sheet profiles | Die investment, sheet thickness, small features, cut deformation and repeatability |
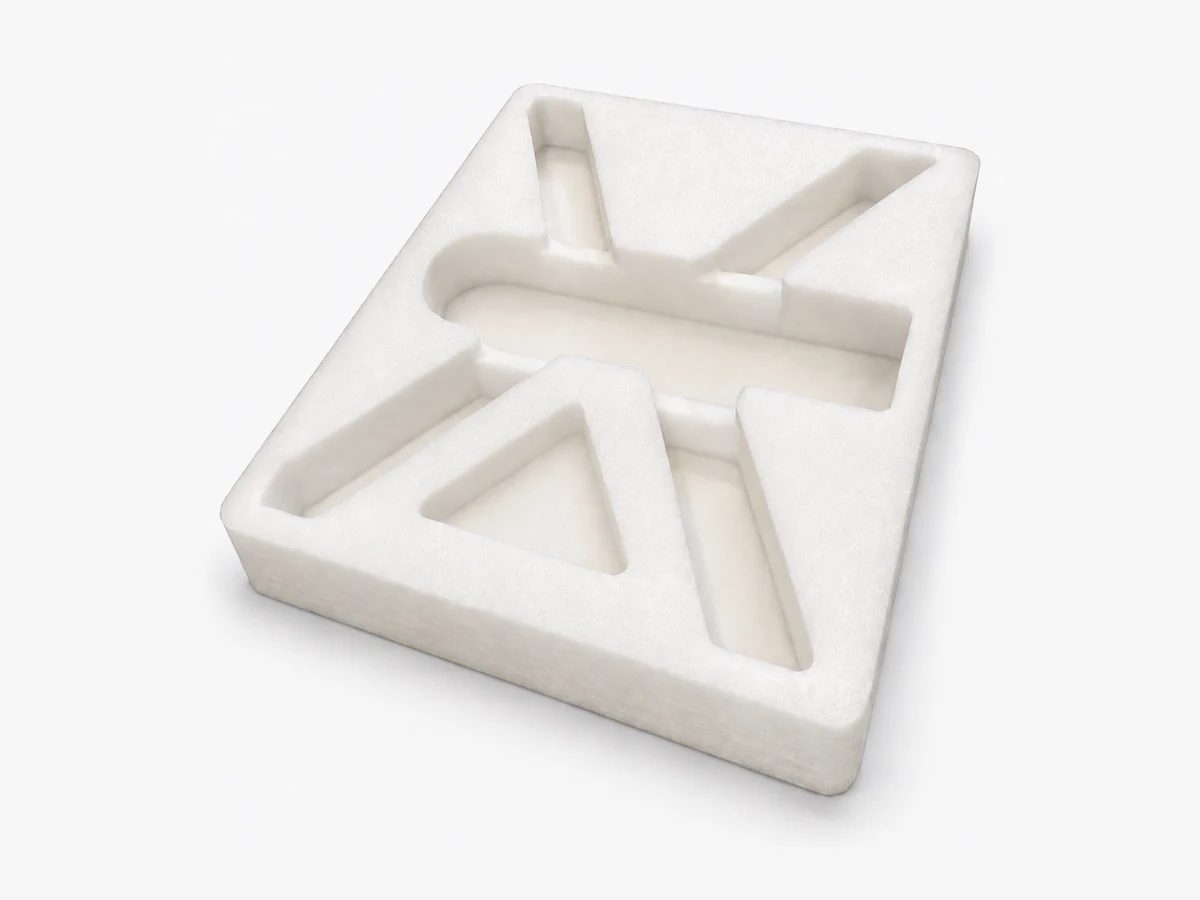
| Glued layers / lamination | Stepped pockets, multi-depth inserts and combined grades | Layer alignment, thickness stack-up, bond strength and adhesive/environment compatibility |
| CNC machining | Pockets, channels and 3D detail in suitable blocks | Tool access, internal radii, fixturing, minimum walls, surface finish and scrap |
| Digital knife cutting / waterjet | Alternative sheet/profile routes where appropriate | Equipment availability, feature quality and any post-cut handling/drying |
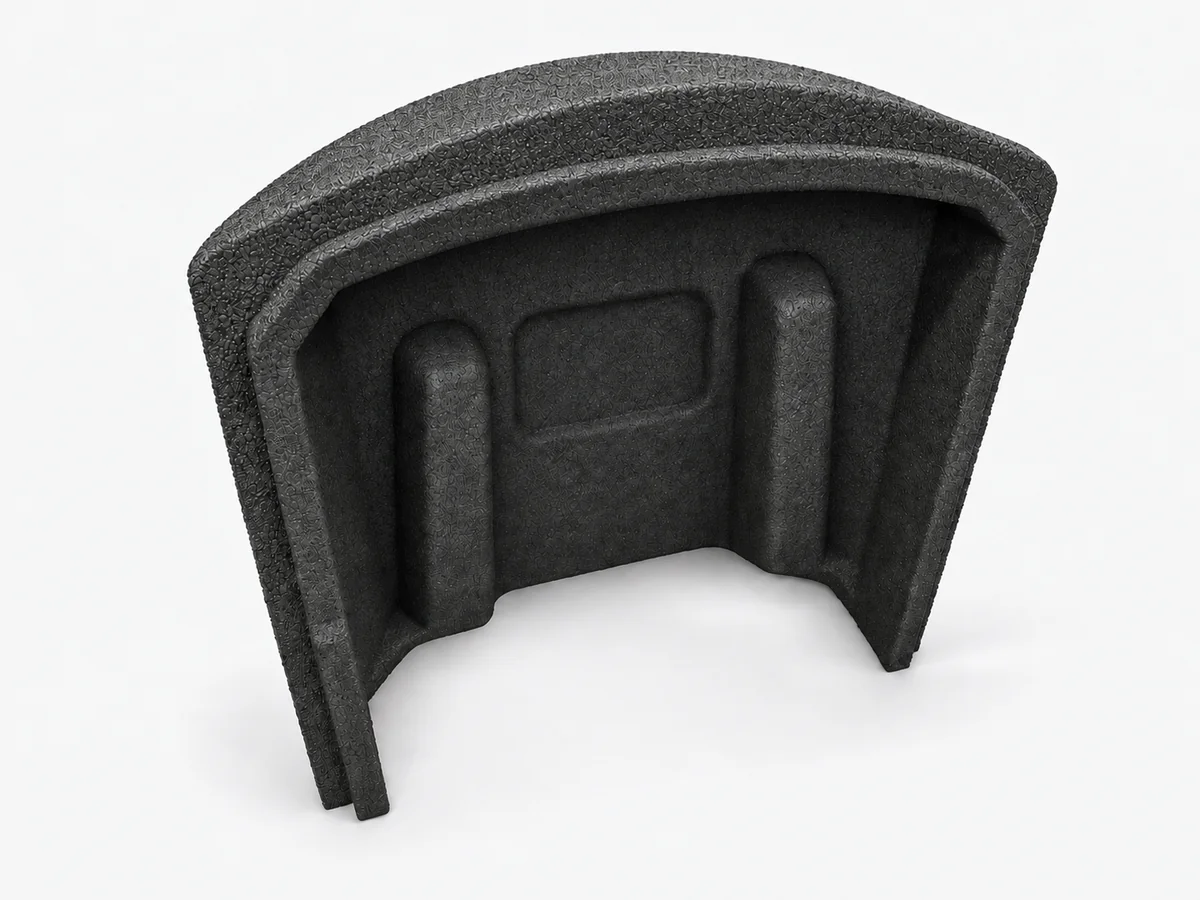
| Thermoforming | Formed liners, panels and shells in compatible sheet grades | Forming window, tooling, local thickness change and springback |
| EPP bead moulding | Repeated shaped parts and integrated features | Tooling, bead fusion, venting, shrinkage, final density and economics at planned quantities |
This is process-selection guidance. FFG’s current examples document CNC machining and die-cut bonded EVA layers; the category also describes thermoformed EVA development. Other routes should be agreed for the actual project. Broader industrial converting routes are described by Zotefoams, sheet processing by Toray, and bead conversion by ARPRO.
PE and PP are challenging surfaces to bond. Select adhesive against the actual foam, joint, loads and environment; prototype the bond rather than choosing glue by polymer name alone. 3M bonding guidance
For purchasing, compare the complete part cost: foam volume, nesting waste, machine time, tooling, assembly, finish, inspection and transport. A layered insert and a machined block can solve similar problems with different cost structures.
Reuse and end-of-life
Ask how many reuse cycles the design must withstand, whether damaged sections can be replaced and where scrap or retired parts will actually go. Sealed Air identifies recycling routes for its non-crosslinked PE foam through facilities accepting LDPE foam; ARPRO identifies recyclability as an EPP property. Local collection, adhesives, mixed-material skins and contamination still need review. Do not apply those claims automatically to every crosslinked or assembled foam product. Sealed Air, ARPRO
6. Potential applications across customer sectors
The following are project ideas to explore with FFG.
| Customer sector | Possible project | Key requirements to define |
|---|---|---|
| Drones, robotics and unmanned systems | Interior supports, cable locators, payload cradles, assembly stands and transport inserts | Mass, fit, heat flow, vibration, electrical/RF interfaces and access |
| Electronics and automation | Sensor kits, controller cases, PCB handling trays and instrument supports | ESD/contact requirements, fragile parts, contamination and tolerances |
| Industrial equipment manufacturers | End caps, spacers, panel liners and service tool kits | Load-bearing areas, creep, chemical exposure and maintainability |
| Optical and test equipment | Survey instrument, camera, lens and calibration kits | Surface protection, cleanliness, extraction force and cushioning |
| Field service, energy and telecom | Organized kits for installers, cable testers and inspection instruments | Repeated handling, glove access, missing-item visibility and case fit |
| Automotive and component logistics | Returnable trays, separators and work-in-progress supports | Reuse cycles, stacking, cleaning and part protection |
| Medical equipment logistics | Instrument or device transport inserts and service kits | Cleaning, contamination, shock and any application-specific qualification; no medical suitability inferred |
| Marine, outdoor and security | Equipment case liners, carried kits and protective interfaces | Moisture, UV where exposed, temperature and repeated use; no qualification inferred |
| Delivery and temperature-sensitive transport | Insulated box liners, payload separators and reusable transport bodies | Complete-system thermal testing, closure and hygiene/contact requirements |
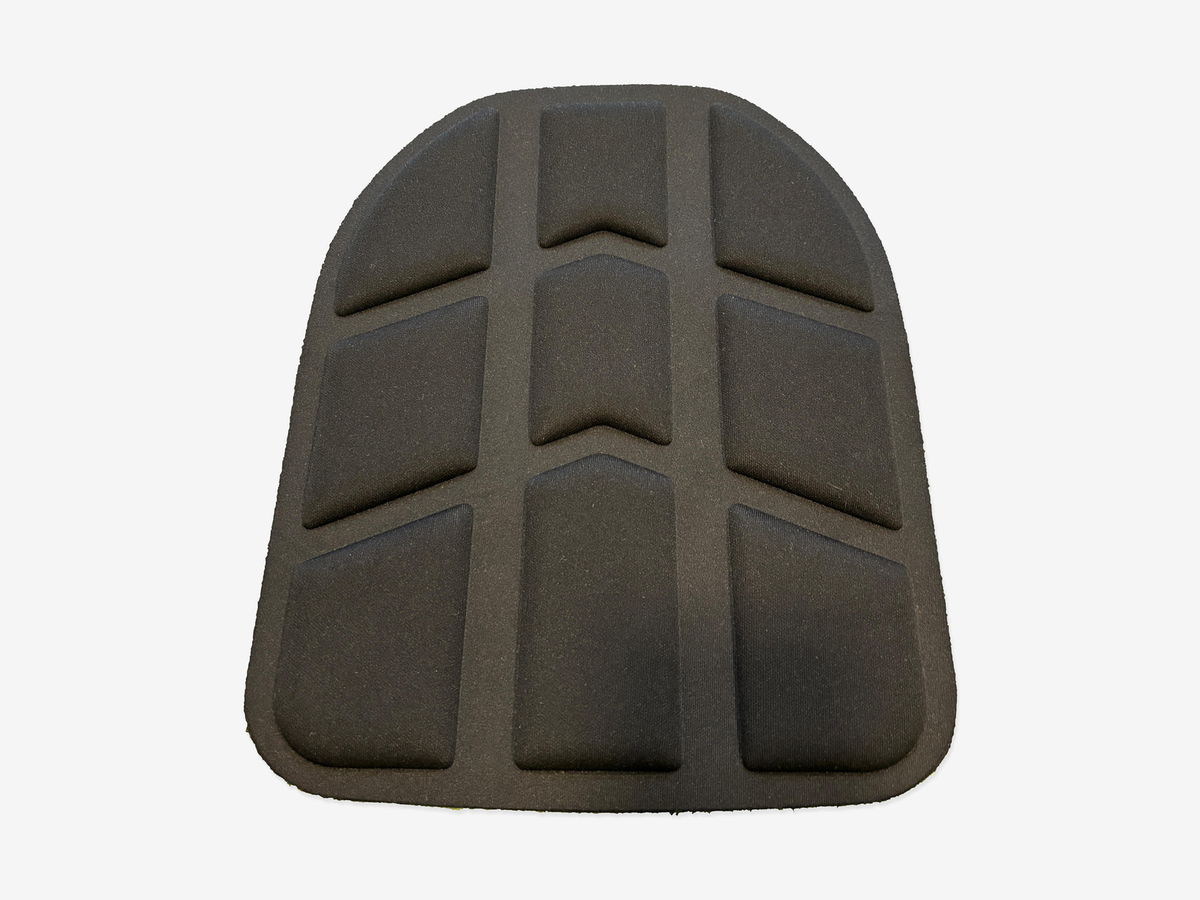
| Textile products and carried equipment | Formed cases, back panels and foam-to-textile assemblies | Comfort, repeated flexing, bonding and attachment details |
7. From a requirement to a verified design
Define the job and acceptance criteria → compare grades and processes → prototype fit, access and bonds → check the complete assembly under relevant exposure → approve the material, drawing and production controls.
For transport packaging, select a test appropriate to the distribution route, equipment and package. A material datasheet does not substitute for the packaged-product test. ISTA test procedures
What to send FFG
Share a drawing, sketch or photos; equipment and enclosure dimensions; equipment mass and foam mass budget; contact surfaces; operating environment; heat/electrical constraints; shock, moisture, ESD or flame requirements; expected quantities and timing. An existing foam specification is useful, but you can also start with the problem you need to solve.
Frequently asked questions
Is EPE different from PE?
EPE is a form of PE foam. Ask whether the supplied material is crosslinked, extruded or bead-based, and identify its grade.
Is higher density always better?
The useful density depends on load, available volume, mass and mechanical response. Compare compression and cushioning data for the actual use.
Can foam protect against humidity?
Water uptake, humidity control and enclosure sealing are different requirements. Define each relevant one.
Can normal black foam protect a PCB from ESD?
Colour is insufficient. Specify and verify the required electrical properties and packaging system.
Can one insert combine multiple foams?
A layered or assembled design can be investigated. Verify the interface, bonds, tolerances and performance of the combined assembly.
Which process should I choose?
Start with geometry, quantity and acceptance criteria. FFG can compare routes as part of the project definition.